

 Send Inquiry
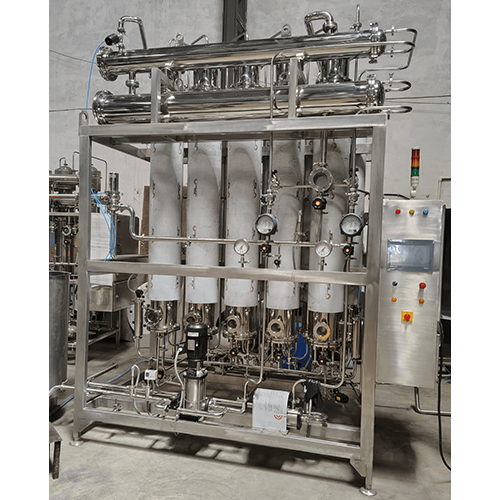
Multi Column Distillation Plant
Multi Column Distillation Plant Specification
- Phase
- Single Phase / Three Phase
- Temperature
- Ambient to 100C (process dependent)
- Frequency
- 50 Hz / 60 Hz
- Usage & Applications
- Purification of water, Pharmaceutical industries, Hospitals, Laboratories, Biotechnology, Electronics, Research Institutes
- Noise Level
- Low (<70 dB)
- Features
- GMP compliant, High purity output, Sanitary construction, Energy efficient, Easy to maintain
- Type
- Multi Column Distillation Plant
- Material
- Stainless Steel (SS 304 / SS 316 as per requirement)
- Capacity
- 50 LPH to 5000 LPH (custom capacities available)
- Computerized
- Yes (Optional/Customizable)
- Control Mode
- Automatic / Semi-Automatic
- Voltage
- 220V / 380V / 415V (as per requirement)
- Power
- 3 kW - 50 kW (depending on size and capacity)
- Weight (kg)
- 550 Kg to 3500 Kg (as per model)
- Dimension (L*W*H)
- Custom / As per specification
- Color
- Metallic Silver/Steel Finish
- Surface Finish
- Electropolished / Mirror finish (GMP standards)
- Feed Water Quality
- Raw, RO, De-mineralized
- Automation
- PLC based control (as per request)
- Pressure
- Atmospheric to 2 bar (as per design)
- Installation Type
- Skid Mounted / Floor Mounted
- Output Conductivity
- Less than 1 S/cm
- Documentation
- Validation & qualification documents provided
- Utility Required
- Electricity, Cooling Water, Feed Water
- Condensate Quality
- Meets IP/BP/USP standards
- Drainage System
- Automatic / Manual drainage system
- Cleaning System
- CIP (Clean-In-Place) provision
- Safety Features
- Over temperature/pressure protection, Dry run protection, Level sensors
- Number of Columns
- 3 to 7 (as required)
- Cooling Type
- Inbuilt Condenser System
Multi Column Distillation Plant Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 100 Units Per Month
- Delivery Time
- 7 Days
- Main Domestic Market
- All India
About Multi Column Distillation Plant
Superior Advantages and Uses
The Multi Column Distillation Plant provides a compelling advantage for pharmaceutical, biotech, electronics, and research sectors, delivering consistently pure water for crucial applications. The top competitive advantages include rapid start-up, minimal maintenance, energy efficiency, and GMP-compliant sanitary design. Used extensively for producing IP/BP/USP-grade distilled water, these systems meet the strictest standards for hospitals and laboratories alike, making them an essential investment for any setting demanding high-purity water.
Export Markets, Delivery, and Payment Terms
Serving a wide domestic market and global clientele, our Multi Column Distillation Plants are dispatched to countries worldwide, including Asia, the Middle East, Africa, and Europe. We provide reliable estimate-based delivery times tailored to each order's specifications and destination. Flexible payment terms are available, ensuring a smooth procurement process. Our efficient logistics enable prompt delivery-both within India and internationally-positioning us as a trusted manufacturer and supplier for diverse industrial requirements.
FAQ's of Multi Column Distillation Plant:
Q: How does a Multi Column Distillation Plant ensure high-purity water output?
A: The plant utilizes multiple distillation columns, advanced automation, and electropolished surfaces to remove impurities, producing water that meets stringent IP, BP, and USP standards. Integrated safety features and quality materials further guarantee consistent purity.Q: What types of feed water can be processed using this system?
A: Our Multi Column Distillation Plant is capable of handling raw, reverse osmosis (RO), and de-mineralized feed water, adapting seamlessly to diverse source qualities while ensuring output conductivity of less than 1 S/cm.Q: When should the plant's clean-in-place (CIP) system be used?
A: The CIP system should be operated according to your standard maintenance schedule or whenever cleaning is necessary to maintain optimum system performance. Automated or manual options make this process simple and efficient.Q: Where are these distillation plants commonly installed?
A: They are widely installed in pharmaceutical industries, hospitals, laboratories, biotechnology companies, electronics manufacturing units, and research institutes needing high-purity water.Q: What is the process for installation and what are the mounting options?
A: Installation can be done as either skid-mounted or floor-mounted, according to your facility's requirements. Comprehensive validation and qualification documentation support a seamless setup process.Q: How does automation improve the plant's operation and safety?
A: PLC-based control systems manage all key functions, offer precise monitoring, and trigger protective actions if issues such as over-temperature, over-pressure, or dry run are detected, ensuring safe and reliable operation at all times.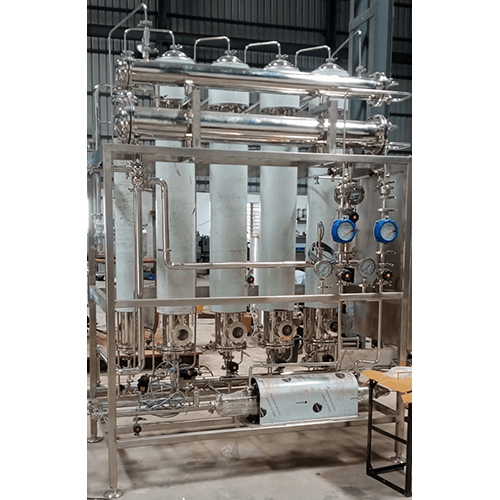

Price:
- 50
- 100
- 200
- 250
- 500
- 1000+

More Products in Pharmaceutical Machinery Category
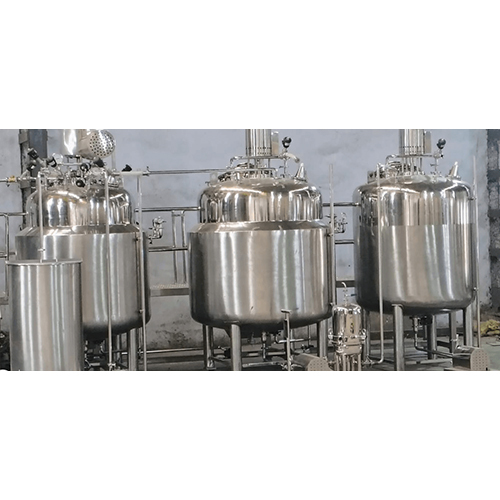
Liquid Oral Manufacturing Plant
Minimum Order Quantity : 1 Unit
Color : Silver/Metallic Finish
Voltage : 220V/380V/415V (as per requirement)
Weight (kg) : Depends on capacity, approx. 300 kg 2500 kg
Control Mode : Other, Automatic/SemiAutomatic
Dimension (L*W*H) : Customized as per plant design
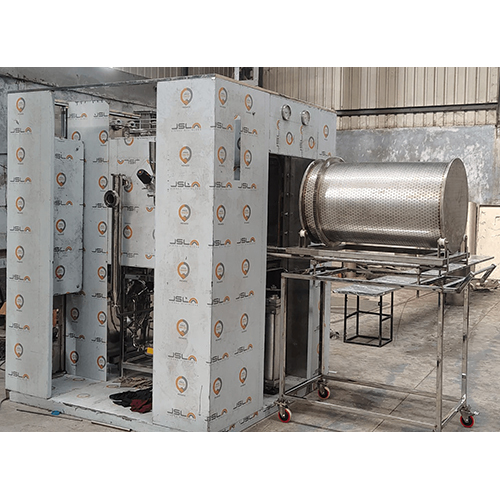
Bung Processor
Minimum Order Quantity : 1 Unit
Color : Metallic Silver
Voltage : 220440 V
Weight (kg) : Variable / As per specification
Control Mode : Automatic
Dimension (L*W*H) : Customizable / As per model
Vertical Sliding Double Door Autoclave
Minimum Order Quantity : 1 Unit
Color : Metallic/Polished Steel Finish
Voltage : 220/380 V
Weight (kg) : 800 to 1500 kg (Approx., Depending on Size)
Control Mode : Other, Automatic PLC based control
Dimension (L*W*H) : Customizable, e.g., 1500 x 1100 x 2100 mm
Super Heated Water Spray Sterilizer
Minimum Order Quantity : 1 Unit
Color : Metallic/Silver
Voltage : 380V / 415V
Weight (kg) : Varies by model (Approx. 20005000 kg)
Control Mode : Other, Automatic/PLC Control
Dimension (L*W*H) : Customized as per requirement (e.g., 4000 x 1800 x 2100 mm)

GST : 24AYMPP8506A1ZI


 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
